Adding value for your metal plate products.


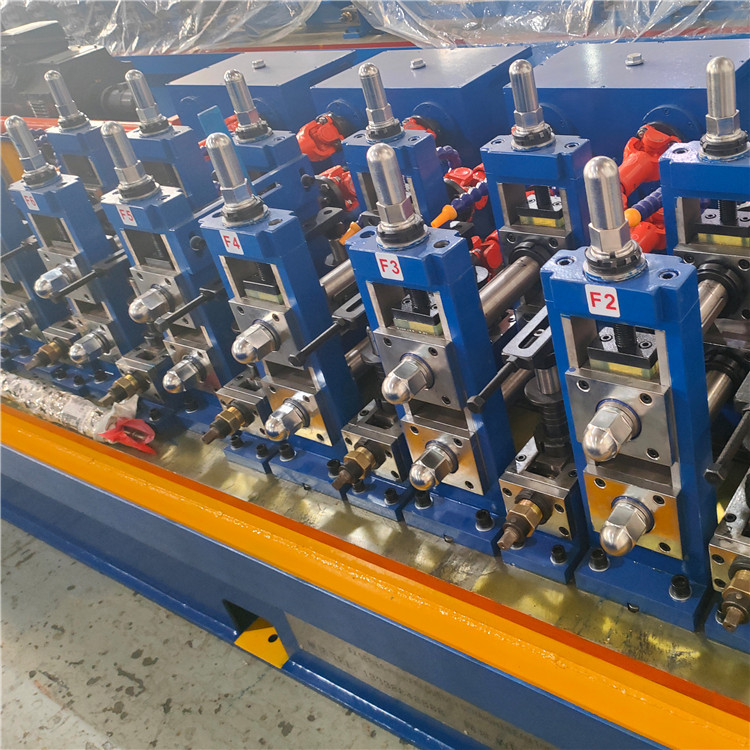
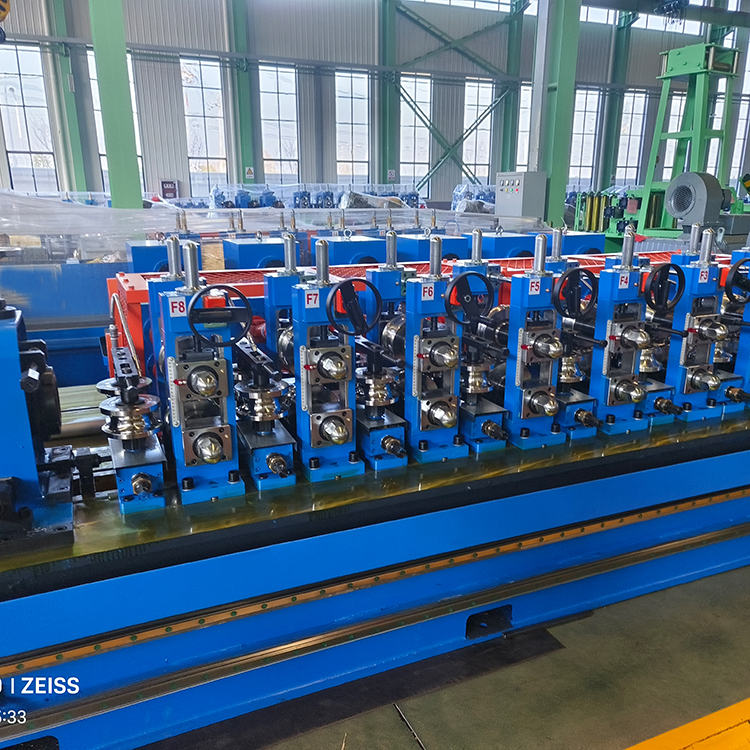
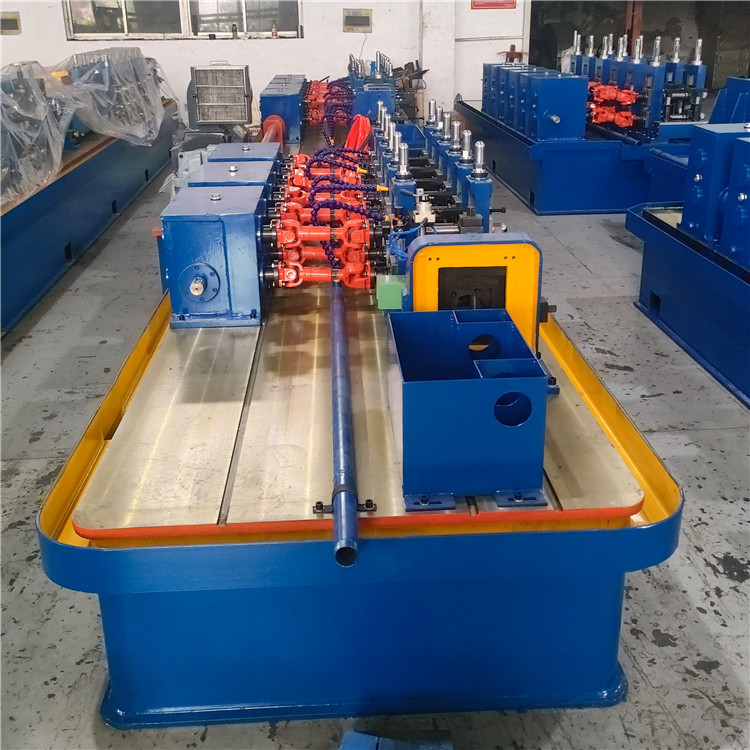
Round Pipe O.D.: 7–25 mm
Round Pipe Thickness: 0.2–1.0 mm
Square Tube Size: 20 × 20 mm
Square Tube Thickness: 0.2–0.8 mm
Reference Line Speed: 20–120 m/min
Main Drive / H.F. Welder: 37 kW / 100 kW
Voltage: 220 / 380 / 415 / 420 / 440 V
Reference Line Weight: Approx. 29,000 kg
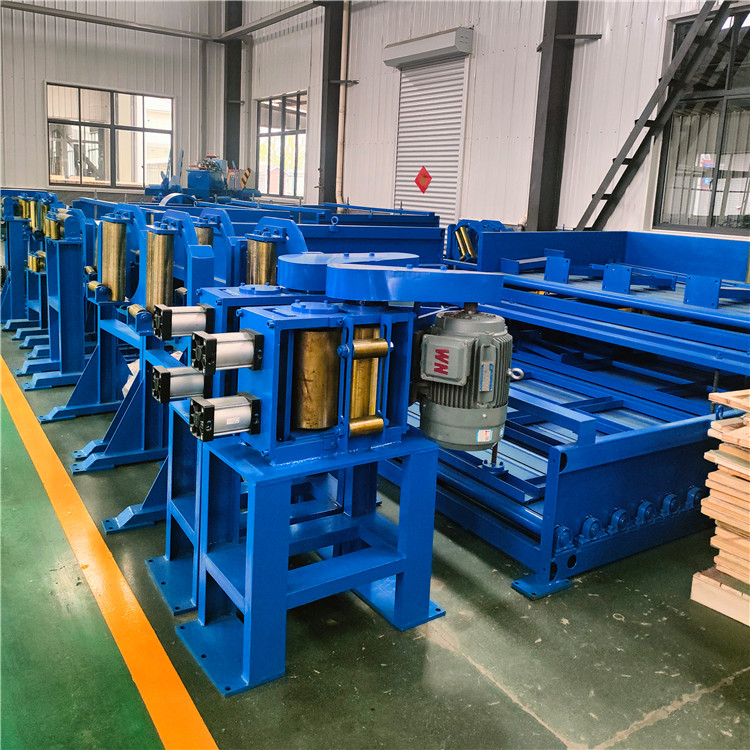
This welded pipe production line is intended for buyers who need more than one finished profile. The line first forms and welds steel strip as a round tube; square or rectangular products require the corresponding sizing arrangement and dedicated roller sets.

Profile selection note: One line does not produce every profile without preparation. The required round, square and rectangular size matrix must be confirmed so that forming and sizing rollers can be included correctly.
| Item | Reference specification |
|---|---|
| Round pipe outside diameter | 7–25 mm |
| Round pipe wall thickness | 0.2–1.0 mm |
| Square tube size | 20 × 20 mm |
| Square tube wall thickness | 0.2–0.8 mm |
| Reference line speed | 20–120 m/min |
| Main drive / high-frequency welder | 37 kW / 100 kW |
| Power supply | 220 / 380 / 415 / 420 / 440 V, configured for the destination |
| Reference line weight | Approx. 29,000 kg |
These are reference values from the current product record. Final output and configuration depend on tube size, wall thickness, material, welding conditions and cut length.
The existing product record specifies a 20 × 20 mm square tube. Any additional square or rectangular dimensions should be included in the technical proposal before the machine and roller scope are finalized.

Strip feeding: steel strip enters from the uncoiler and strip-preparation equipment.
Round-tube forming: forming stands progressively shape the strip before welding.
Longitudinal welding: the prepared edges are welded to produce a continuous tube.
Profile sizing: dedicated sizing rollers control round dimensions or convert the welded tube into square or rectangular profiles.
Length cutting: the finished section is cut according to the order.


Supports the coil and feeds steel strip into the line. Capacity and expansion method are selected according to coil data.

Trims and joins consecutive strip ends to prepare continuous feeding through the production line.

Roll stands progressively form the strip before high-frequency welding closes the longitudinal seam.

Controls the final geometry and dimensions. The roller arrangement is matched to the ordered round or square tube range.

Cuts continuously produced tube to the ordered length. The solution is selected around line speed and product range.

The roller plan is a central part of a multi-profile project. Buyers should list all target dimensions so the supplier can review roller sharing, dedicated roller sets and the expected changeover work.
separate required round, square and rectangular dimensions;
state wall thickness for every profile, not only the maximum value;
confirm whether products use black steel or pre-galvanized strip;
define finished lengths and the required cutting method;
allow workshop space for roller storage and maintenance.

Round welded tubes are commonly selected for general fabrication, furniture, light structures and other downstream processing. Square and rectangular tubes are often chosen where flat faces simplify joining or frame construction. Suitability for a regulated pipe standard must be reviewed separately against the required material, testing and certification scope.
To prepare a useful technical proposal, please provide:
tube shapes and minimum/maximum dimensions;
wall-thickness range and raw-material grade;
coil width, coil weight and strip condition;
finished cut length and target output;
factory voltage, frequency and phase;
available workshop length and layout restrictions.

The confirmed technical proposal should define the equipment list, electrical requirements, roller scope, line layout, inspection items, installation support and spare-parts requirements. This avoids treating optional equipment as part of every standard line.


It can be designed for multiple profiles when the required sizing arrangement and roller sets are included. Send the complete profile matrix before configuration.
No. Compliance with a particular pipe standard depends on material, process control, testing and certification requirements. This page does not claim API compliance without a confirmed project specification.
Changeover depends on the mill design, roller-sharing plan, number of stands, tooling method and operator procedure. It should be evaluated for the selected configuration rather than quoted as one universal time.
Send all required round, square and rectangular dimensions, together with wall thickness and material, so the roller and equipment scope can be reviewed.
Email: admin@tsshuoen.com | WhatsApp: +86 193 3157 2740

ERW Steel Pipe Making Machine for Round and Square Tubes

High-Speed ERW Carbon Steel Tube Mill
ERW Pipe Production Line for Round, Square and Rectangular Tubes
High Frequency ERW Pipe Making Machine for Carbon Steel Tubes
TEMP ERW CREATE CHECK DELETE

 +86 19331572740
 +86 19331572740
 admin@tsshuoen.com
