Adding value for your metal plate products.


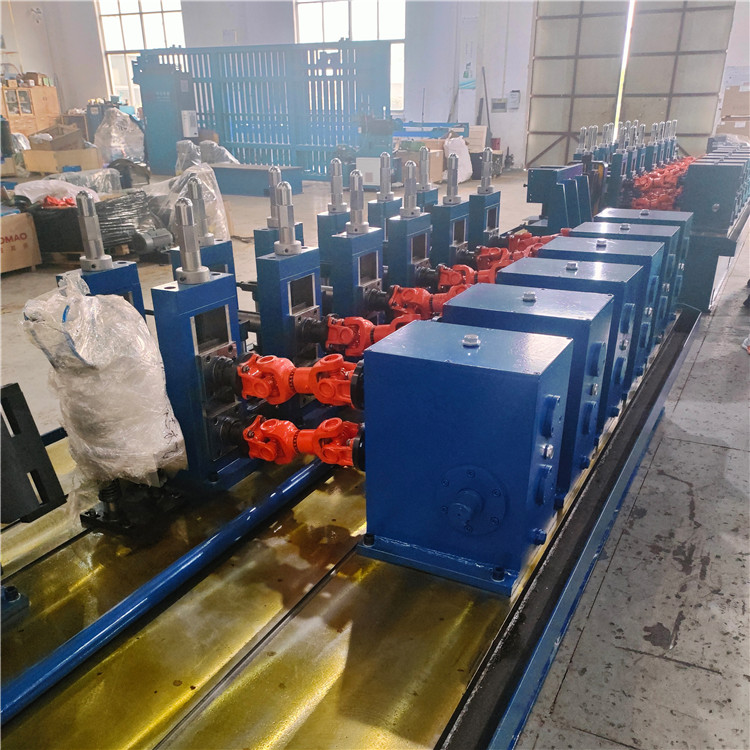
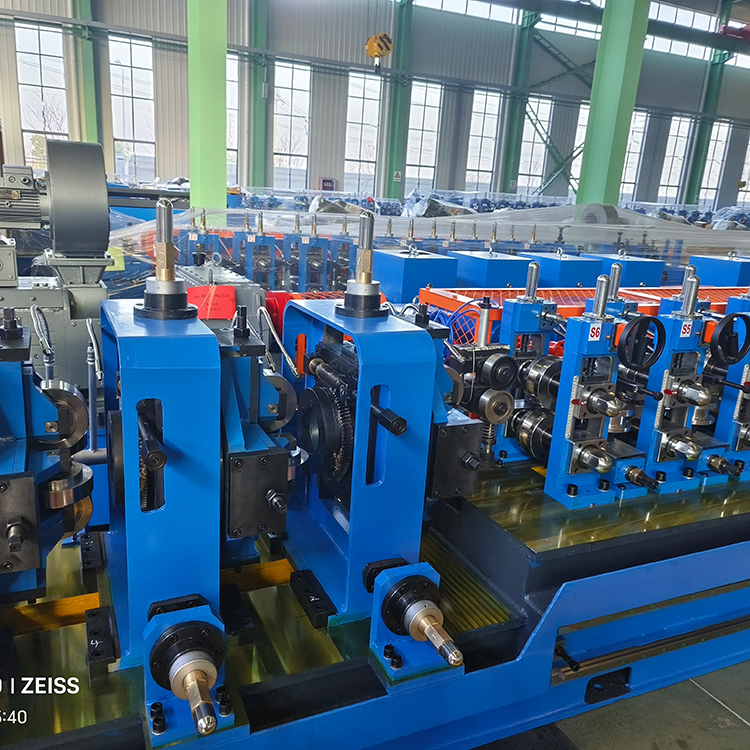
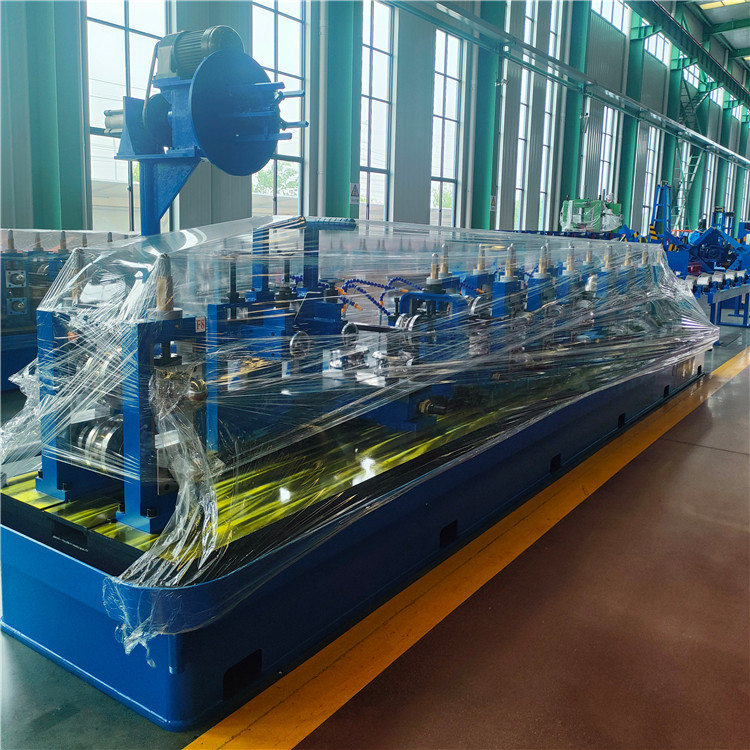
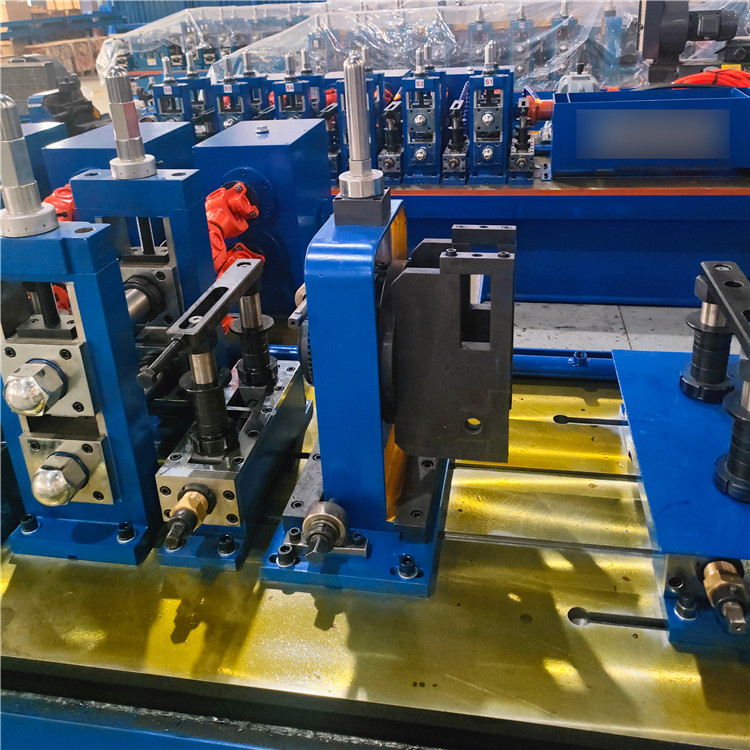
Round Pipe O.D.: 7–25 mm
Round Pipe Thickness: 0.2–1.0 mm
Square Tube Size: 20 × 20 mm
Square Tube Thickness: 0.2–0.8 mm
Reference Line Speed: 20–120 m/min
Main Drive / H.F. Welder: 37 kW / 100 kW
Voltage: 220 / 380 / 415 / 420 / 440 V
Reference Line Weight: Approx. 29,000 kg
This ERW tube mill forms steel strip into longitudinally welded round pipe and, with the corresponding sizing rollers, square tube. It is intended for small-diameter welded tube production. The final machine configuration is selected according to the required tube dimensions, wall thickness, material and target output.

Selection note: The values below are the specifications currently listed for this model. Production speed, installed power and equipment layout are finalized according to the requested pipe range and production plan.
| Item | Reference specification |
|---|---|
| Round pipe outside diameter | 7–25 mm |
| Round pipe wall thickness | 0.2–1.0 mm |
| Square tube size | 20 × 20 mm |
| Square tube wall thickness | 0.2–0.8 mm |
| Reference line speed | 20–120 m/min |
| Main drive / high-frequency welder | 37 kW / 100 kW |
| Power supply | 220 / 380 / 415 / 420 / 440 V, configured for the destination |
| Reference line weight | Approx. 29,000 kg |
Actual production speed depends on tube size, wall thickness, material grade, welding conditions and cut length. The confirmed technical proposal governs the supplied line.

Uncoiling: steel strip is released from the coil and guided into the line.
End preparation and joining: the tail of one coil and the head of the next coil are trimmed and joined for continuous feeding.
Forming: roll stands progressively form the flat strip into an open round tube.
High-frequency welding: the strip edges are heated and pressed together to create the longitudinal weld.
Sizing: sizing stands control the final tube geometry and dimensions.
Cutting: the finished tube is cut to the ordered length for collection and further processing.


Supports the steel coil, expands to hold it and feeds the strip into the production line. Coil loading capacity and expansion method are matched to the selected line.

Trims the strip ends and joins consecutive coils. This prepares a smoother connection before the strip continues to the forming section.

A sequence of roll stands gradually forms the steel strip into a round tube profile before welding. Roll design is developed around the required product range.

Controls the final outside dimensions and tube geometry after welding and cooling. Square tube production requires the corresponding sizing arrangement and roller set.

Cuts the continuously produced tube to the specified length. The cutting solution is selected according to tube size, line speed and finished-length requirements.

The line can be configured around the buyer’s product plan instead of using one fixed specification for every project. Items commonly reviewed during selection include:
round pipe or square tube dimensions and wall thickness;
carbon steel, black steel or pre-galvanized strip as applicable;
coil width, coil weight and material grade;
required production speed and finished cut length;
plant voltage, frequency and electrical standard;
roller sets, cutting method, line layout and machine color.


For an accurate model selection and quotation, please send:
tube shape: round, square or rectangular;
minimum and maximum tube dimensions;
wall-thickness range;
raw-material grade and coil information;
required finished length and target output;
local voltage, frequency and phase;
available workshop space or preferred line layout.

Before shipment, the agreed equipment configuration, main assemblies and available test records should be checked against the confirmed technical proposal. Installation, commissioning, operator training and spare-parts requirements can be discussed as part of the project scope.


A line may produce round pipe and square tube when it is designed with the appropriate forming or sizing arrangement and matching roller sets. Please provide both product ranges before the configuration is finalized.
No. This is a reference line-speed range. Actual output varies with tube diameter, wall thickness, material, welding stability and cutting requirements.
Voltage and frequency can be configured for the destination, and machine color can be discussed before production.
Please provide tube shape, size range, wall thickness, material grade, finished length, target output and local power supply. These details allow the technical team to select a suitable line.
Send your pipe dimensions, wall thickness, material and production target. We will use these requirements to prepare a suitable configuration for discussion.
Email: admin@tsshuoen.com | WhatsApp: +86 193 3157 2740
ERW Steel Pipe Making Machine for Round and Square Tubes

High-Speed ERW Carbon Steel Tube Mill

ERW Pipe Production Line for Round, Square and Rectangular Tubes
High Frequency ERW Pipe Making Machine for Carbon Steel Tubes
TEMP ERW CREATE CHECK DELETE

 +86 19331572740
 +86 19331572740
 admin@tsshuoen.com
